MX-5050B Maintenance Manual — Digital Edition · Part 2 · scan pages 12-22
Routine Maintenance and Conversion Information
2-1 ROUTINE MAINTENANCE↑ TOP
It is important that routine maintenance be performed at the recommended intervals. External cleaning and demagetization procedures should be performed after each eight hours of operation, and the interior of the transport should be cleaned once a month. The lubrication procedure should be performed after 1,000 hours of operation or after 6 months, whichever comes first.
2-1-(1) CLEANING↑ TOP
Oxide particles from the magnetic tape tend to collect on components in the tape path and degrade the performance of the recorder. To clean the head assembly, proceed as follows:
- Disconnect the power cable from the power supply.
- Lift the head cover as shown in Fig. 2-1. CAUTION
WHEN CLEANING THE HEADS, USE ONLY THE RECOMMENDED SOLVENT (HEAD CLEANER) TO AVOID DAMAGING THE HEADS. KEEP THE HEAD CLEANER OFF PLASTIC FINISHES AND THE CAPSTAN PINCH ROLLER. DO NOT USE METAL TOOLS THAT CAN SCRATCH THE HEADS.
-
Clean each head stack thoroughly with a cotton-tipped applicator (Q tip) dampened with head cleaner.
-
Use isopropyl alcohol to clean all tape-guiding components, the capstan shaft, and the capstan pinch roller.
CAUTION
-
DO NOT USE A HEAD CLEANER ON THE CAPSTAN PINCH ROLLER AS DAMAGE WILL RESULT AND THE TAPE WILL SLIP.
-
BEFORE REMOVING THE REAR COVER, THE PLUG MUST BE DISCONNECTED FROM THE POWER SUPPLY TO AVOID AN ELECTRIC SHOCK.
-
Remove the rear cover of the recorder by removing 6 screws(Refer to Fig.3-1).
-
Use a vacuum cleaner and a small brush to remove all dust or contamination from the interior of the transport. If necessary lightly moisten brush with isopropyl alcohol to clean parts.
-
Install the rear cover.
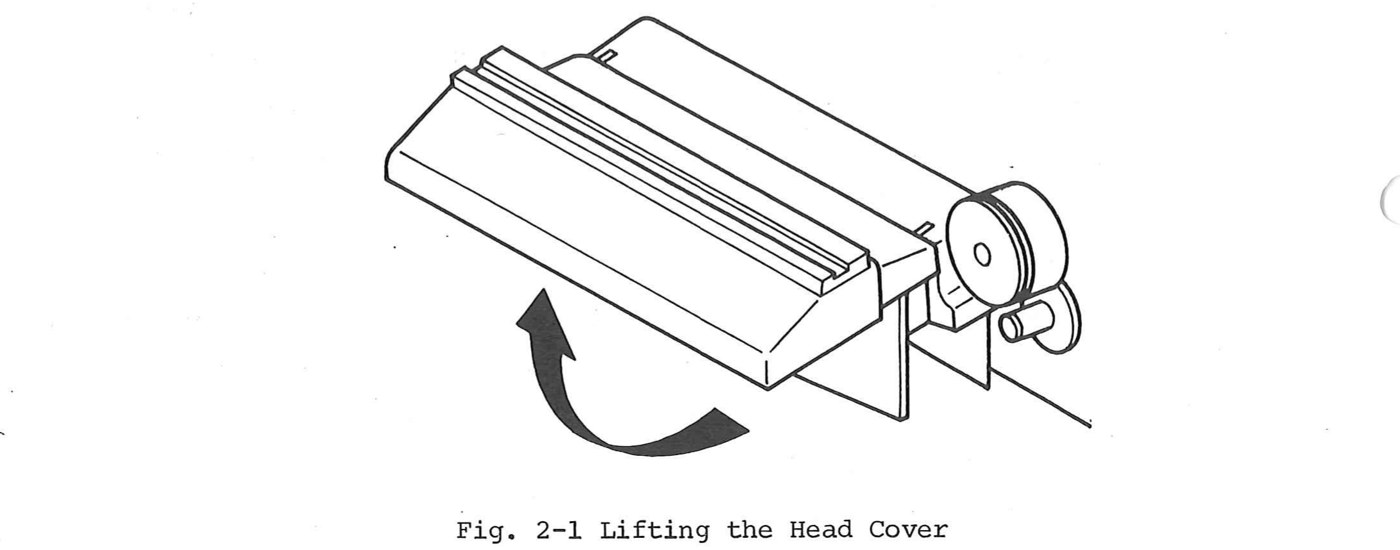 ⤢ zoomFig. 2-1 Lifting the Head Cover: the hinged head cover tilted up and away from the head assembly, an arrow curving to show the way it swings
2-1-(2) DEMAGNETIZING↑ TOP
The heads and tape guiding components in the tape path should be demagnetized after each eight hours of operation. These components can acquire permanent magnetization that increases signal noise and distortion and partially erase high frequencies on recorded tape. Use a hand-held head demagnetizer to demagnetize all components in the tape path as follows:
-
Turn equipment power off and move any recorded tape near the transport away (tape could be partially erased by the demagnetizer).
-
Lift the head cover as shown in Figure 2-1
-
Cover the demagnetizer tips with adhesive tape to prevent scratching the head stacks.
-
With the demagnetizer held away from the transport, connect the demagnetizer to a power source.
-
Slowly move the demagnetizer tips close to the head, lightly touch the demagnetizer tips to the face of one head stack and slowly move the tips up and down the stack several times. Then slowly withdraw the demagnetizer as shown in Fig. 2-2
-
Repeat step 5 for each head stack.
-
Repeat the motions in step 5 for each guide and other metallic parts in the tape path.
-
Move the demagnetizer slowly away from the transport to at least three feet and then disconnect the power from the demagnetizer.
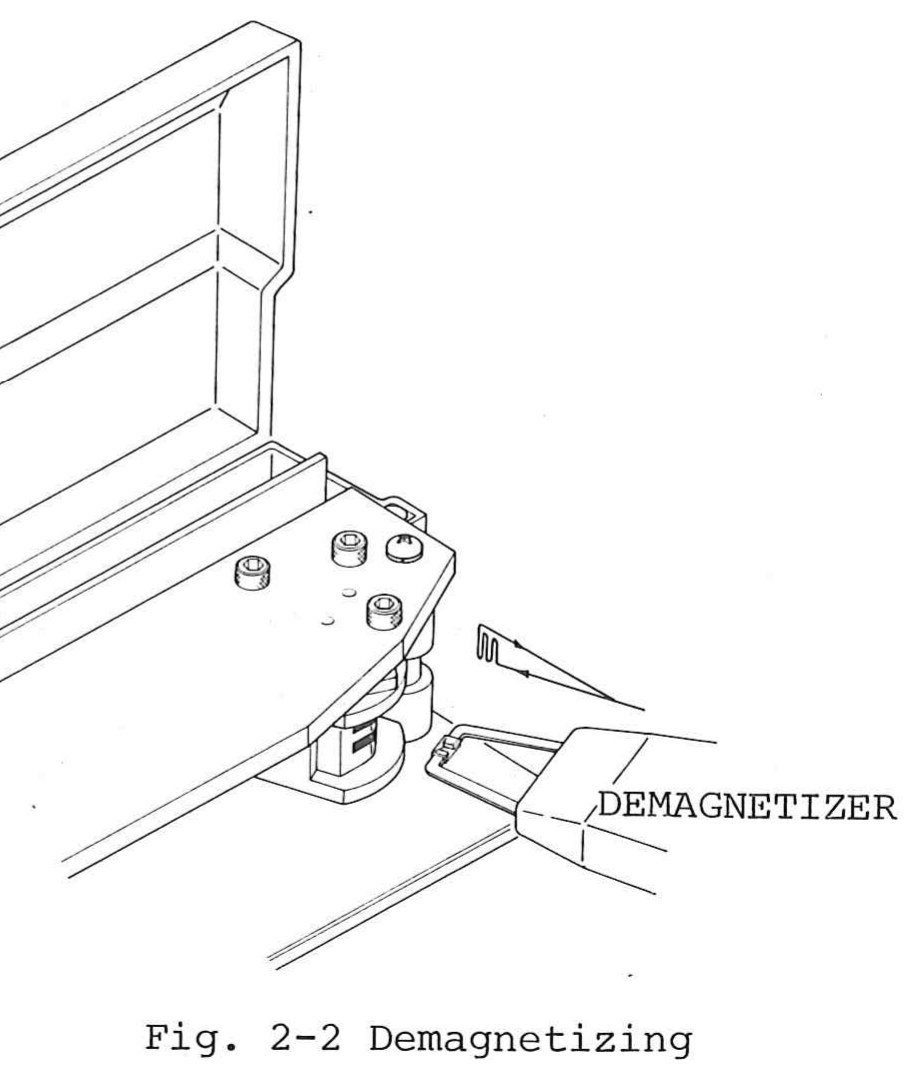 ⤢ zoomFig. 2-2 Demagnetizing: a demagnetizer drawn slowly back from the head stack inside the open head cover, its body labelled DEMAGNETIZER
2-1-(3) LUBRICATION↑ TOP
The only components requiring lubrication are the capstan sleeve bearing, the guide roller bearing, and the capstan pinch roller bearing. Refer to Fig. 2-3 and proceed as follows:
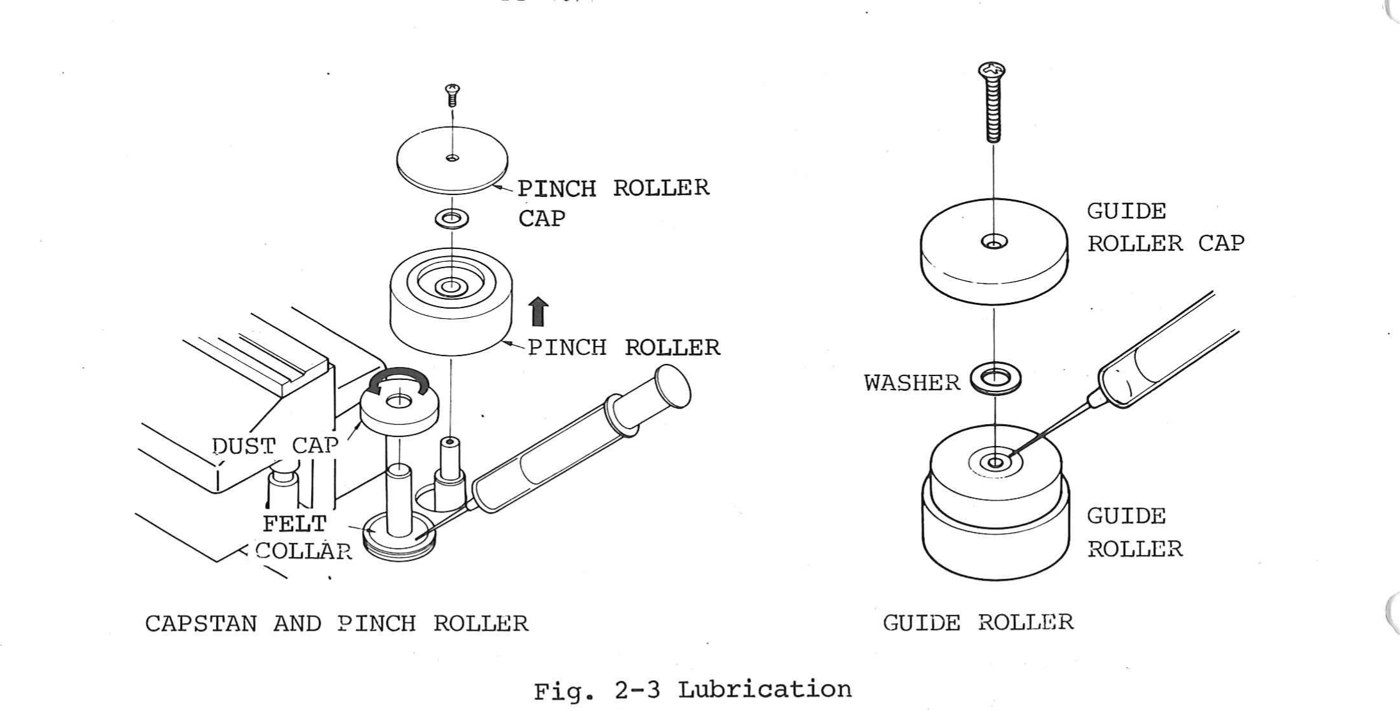 ⤢ zoomFig. 2-3 Lubrication: two exploded views — at left the capstan and pinch roller with the pinch roller cap, dust cap and felt collar, at right the guide roller with its cap and washer — each being oiled from a needle oiler
CAUTION
-
DO NOT USE ANY OIL EXCEPT ANDEROL #456 FOR LUBRICATION.
-
BE CERTAIN TO CLEAN THE CAPSTAN SHAFT THOROUGHLY. LUBRICATING OIL CAN RUIN THE CAPSTAN PINCH ROLLER AND MAGNETIC TAPE. CLEAN THE CAPSTAN, PINCH ROLLER, AND GUIDE ROLLER WITH ISOPROYL ALCOHOL, AFTER LUBRICATION.
For the pinch roller bearing and the capstan sleeve bearing:
-
Remove the pinch roller cap by removing the screw on it.
-
Remove the pinch roller from the pinch roller shaft. Note that there are two polyslider washers on both sides of the pinch roller bearing.
-
Remove the metal dust cap from the capstan shaft by turning it counter-clockwise.
-
The felt collar is now visible. Apply 2 or 3 drops of oil to this felt collar. Do not over lubricate.
-
Apply a few drops of oil to the pinch roller bearing.
-
Wipe off any excess oil and install the dust cap and pinch roller cap. Fig. 2-3 Lubrication
For the guide roller bearing
- Remove the guide roller cap by removing the screw on the cap as shown in Fig. 2-3.
- Apply a few drops of oil to the guide roller bearing.
- Wipe off any excess oil and install the guide roller cap.
2-2 TAPE REPLACEMENT↑ TOP
The MX-5050B is set at the factory for Scotch #206 Recording Tape. If another tape is to be used, the following adjustment may be required for the optimum performance of the tape. Refer to Section 4. Required adjustments are:
- The record bias adjustment.
- The record level set for NAB equalization.
- The record level adjustment.
2-3 EQUALIZER CHANGE↑ TOP
The equalizer between the NAB or the IEC can be changed by means of the EQUALIZER switch (SW505) on the back panel.
However, a fine equalizer adjustment and a record level set made by the RECORD LEVEL switch are required.
Refer to Section 4 to aid the fine adjustment.
-
Set the EQUALIZER switch on the back panel to the desired position IEC or NAB.
-
On IEC equalization, set the RECORD LEVEL switch to "H" 320nWb/m reference recorded level On NAB equalization, set the RECORD LEVEL switch to the appropriate position depending on the capability of the tape being used. Refer to Table 2-1 for RECORD LEVEL set on NAB equalization.
Table 2-1 Record level switch position
| Position | Flux | Relative level. | Test Tape | Recording tape to be used |
|---|---|---|---|---|
| Low | 185 nWb/m* | 0 dB | Ampex Operating level | Scotch 177, Ampex 641 |
| Medium | 250 nWb/m* | +2.6 dB | MRL NAB Reference flux | Scotch 206, 207, 250 Ampex 406, 407, 456 |
| High | 320 nWb/m** | +3.8 dB | BASF or MRL IEC Standard | IEC Equalization |
- Short circuit flux Open circuit flux
FREQUENCY CONVERSION
On the direct-drive capstan version, frequency conversion is not required. Frequency conversion is performed by changing the drive pulley and the wiring on the starting capacitor p.c.b. as follows. Required parts are listed in Table 2-2.
- Place the transport in an upright position and remove the rear cover.
- Remove the capstan drive belt from the drive pulley.
- Loosen the two hexagonal socket-head screws on the drive pulley and remove it.
- Insert the required drive pulley to the motor shaft, adjust the height of the drive pulley to the same height as the capstan fly-wheel, and tighten the two hexagonal socket-head screws.
- Install the capstan drive belt.
- Resolder the lead wire on the starting capacitor p.c.b. as shown is Fig2-4. Table 2-2 Required parts
| Model | MX-5050B-2H | MX-5050B-2L,4L |
|---|---|---|
| Tape speed | 15 and 7 1/2ips | 7 1/2 and 3 3/4ips |
| Line frequency | 50Hz | 60Hz |
| Otari Part No. | Pulley | KCOD010 |
| Belt | BE2M140 | |
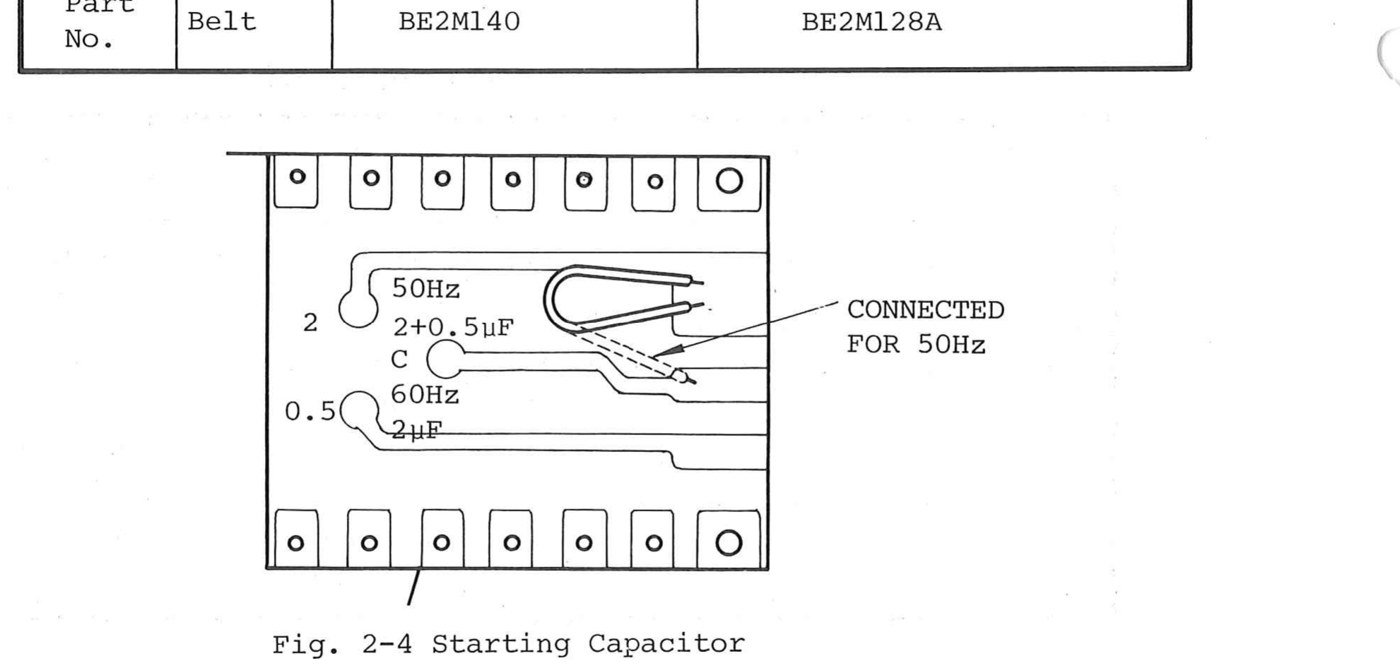 ⤢ zoomFig. 2-4 Starting Capacitor: the starting capacitor terminal board, its 50Hz and 60Hz taps marked 2+0.5 µF and 2 µF, with a lead shown connected for 50 Hz |
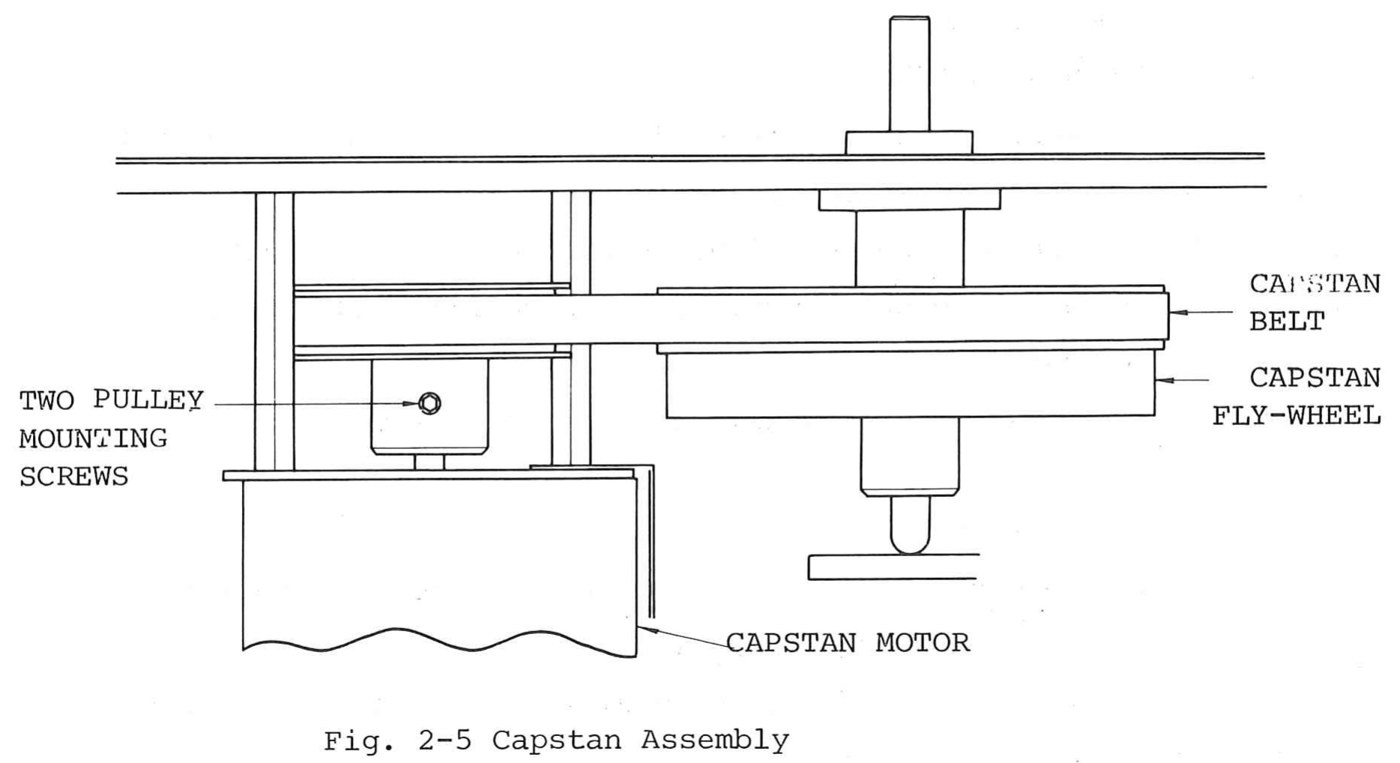 ⤢ zoomFig. 2-5 Capstan Assembly: a side view of the capstan drive: the motor below, the belt running up to the flywheel, and the two pulley mounting screws called out at the left
2-5 LINE VOLTAGE CONVERSION↑ TOP
The line voltage is converted by resoldering the wiring on the junction terminals.
- Remove the rear cover by removing six cross-head screws.
- Resolder the lead wire of the voltage selection terminal on the junction terminals to the desired voltage terminal marked as shown in Fig. 2-6.
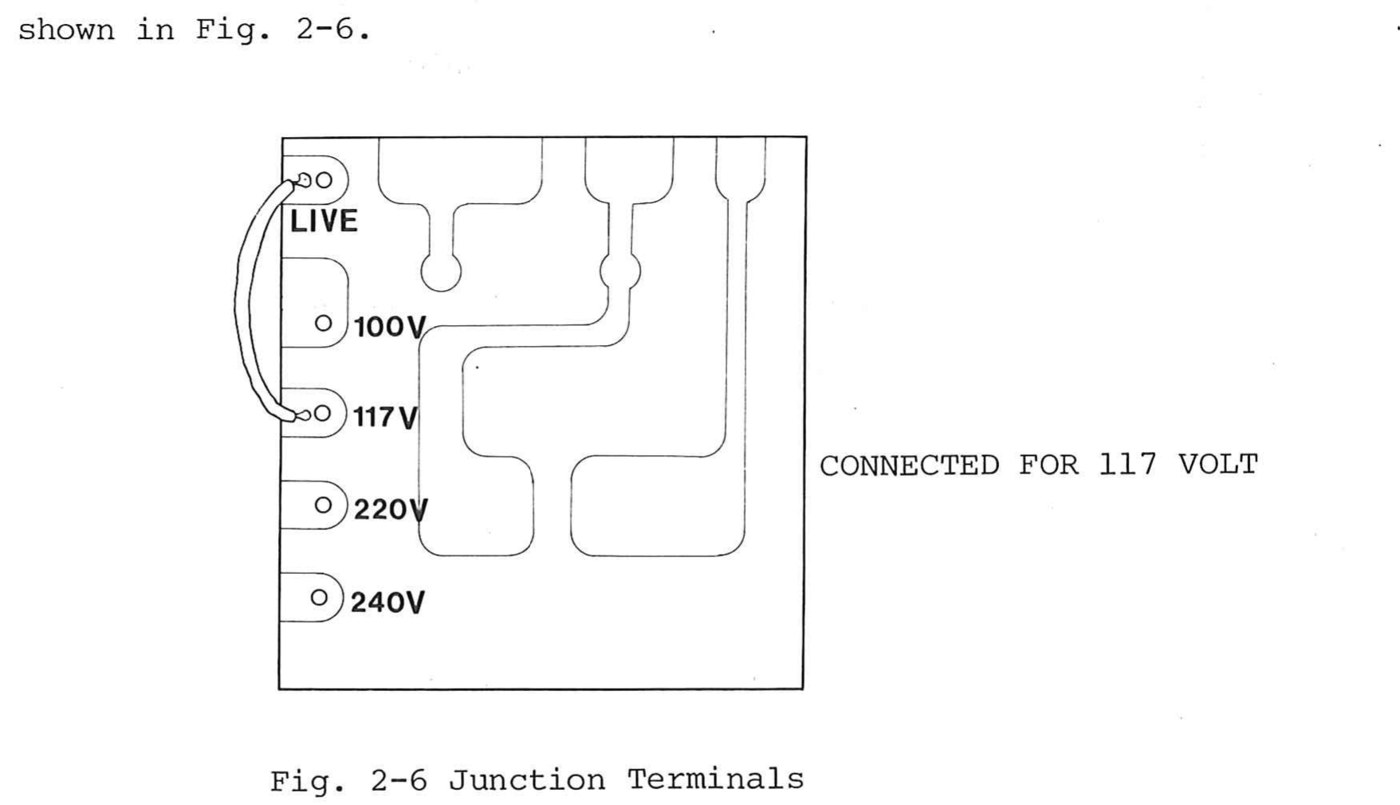 ⤢ zoomFig. 2-6 Junction Terminals: the junction terminal board with LIVE, 100V, 117V, 220V and 240V tags, strapped for 117 volts
2-6 TAPE SPEED CONVERSION↑ TOP
2-6-(1) DC SERVO CAPSTAN MOTOR MODEL↑ TOP
Tape speed conversion on the direct drive capstan model can only be made by placing the speed conversion switch (SW701), as shown in Fig. 2-7, to the desired position, as well as the equalization switch. However, fine adjustment of the equalizer and a tape speed test are necessary. Refer to Section 4 for the equalizer fine adjustment, and for the tape speed test.
-
Remove the rear cover.
-
Place the speed conversion switch to the desired position by using a minous-head screw driver.
-
Adjust the reproduce and record equalizer, and the tape speed as necessary.
CONTROL P.C.B.
H L HIGH VERSION LOW VERSION SW701
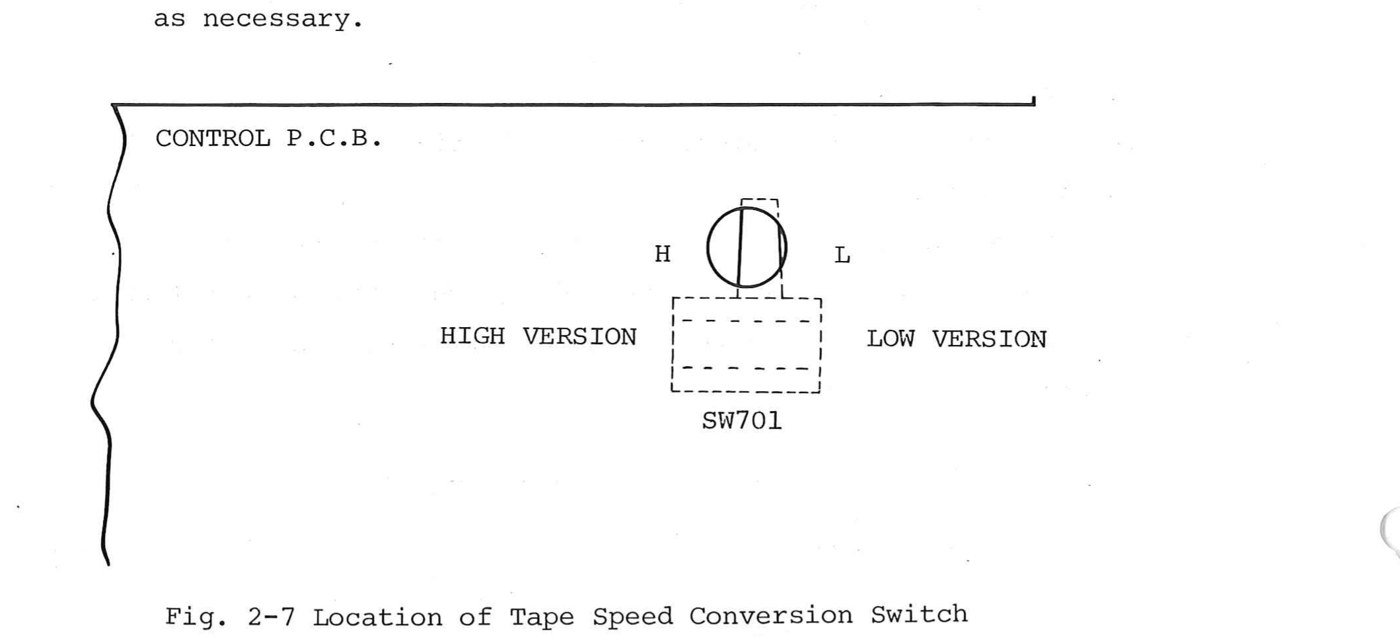 ⤢ zoomFig. 2-7 Location of Tape Speed Conversion Switch: the control p.c.b. with speed conversion switch SW701 between its H and L positions, marked HIGH VERSION and LOW VERSION
2-6-(2) HYSTERESIS SYNCHRONOUS MOTOR MODEL↑ TOP
On the hysteresis synchronous motor driven capstan model, drive pulley and drive belt replacement, and speed conversion switch set are necessary.
Refer to Table 2-2 for the required parts.
After the tape speed conversion, fine adjustment of the equalizer is necessary.
- Place the transport in an upright position and remove the rear cover.
- Place the speed conversion switch(SW701) to the desired position by using a minous-head screw driver (refer to Fig. 2-7).
- Remove the capstan drive belt from the drive pulley.
- Loosen the two hexagonal socket-head screws on the drive pulley and remove it.
- Insert the required drive pulley to the motor shaft, adjust the height of the drive pulley to the same height as the capstan fly-wheel, and tighten the two hexagonal socket-head screws.
- Install the capstan drive belt.
- Adjust the reproduce and record equalizer as necessary.
2-7 FUSE REPLACEMENT↑ TOP
If a fuse is blown, check the cause and repair it.
CAUTION
FOR CONTINUED PROTECTION AGAINST FIRE HAZARD, REPLACE ONLY WITH THE SAME TYPE OF FUSE. BEFORE REPLACING THE FUSE, REMOVE THE POWER CORD FROM THE POWER SOURCE.
Information concerning the seven fuses can be found in Table 2-3.
For the main power fuse (FS801), proceed as follows:
- Remove the side board on the left by removing four hexagonal socket-head screws.
- Replace the main power fuse (FS801) on the power switch p.c.b.
- Re-install the left side board. SW804 EDIT SW803 REEL SW802 SPEED SW801 POWER FS801 2A POWER SWITCH P.C.B.
Fig. 2-8 Main Power Fuse Location
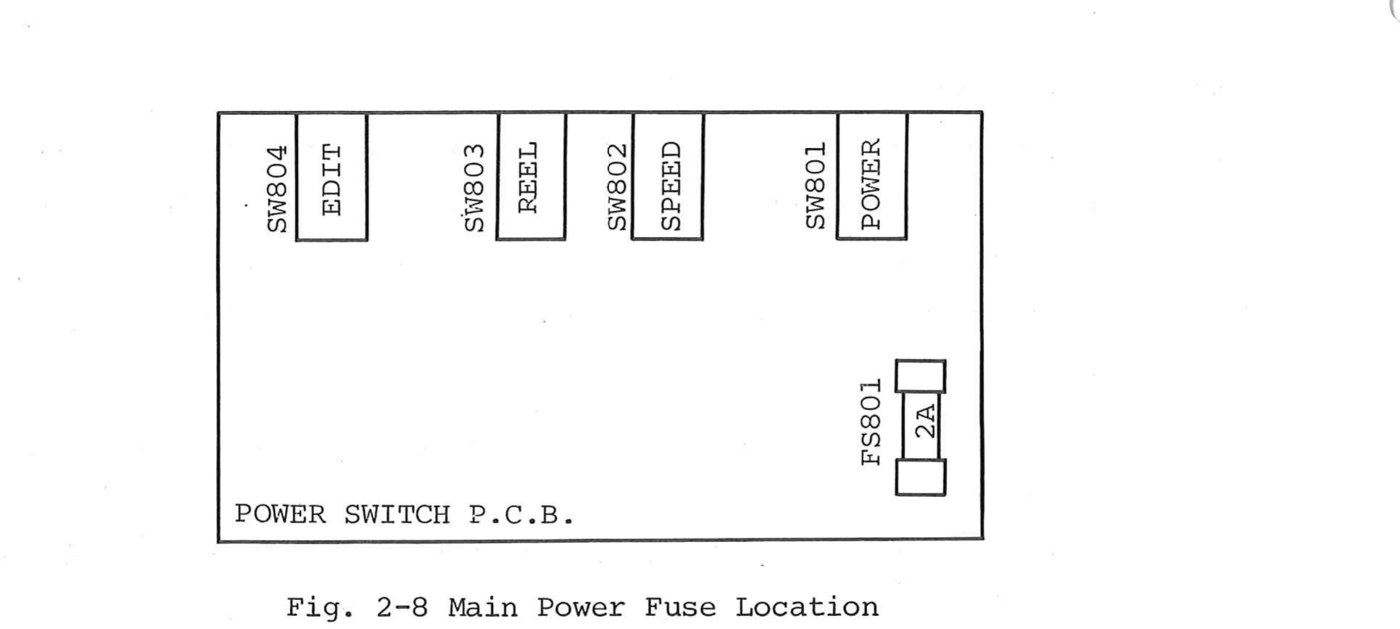 ⤢ zoomFig. 2-8 Main Power Fuse Location: the power switch p.c.b. carrying SW801 to SW804 for power, speed, reel and edit, with the 2A main fuse FS801 at the right
For other fuses (FS701~706), proceed as follows:
- Remove the rear cover by removing six cross-head screws.
- Remove six screws marked "OPEN" on the control p.c.b.
- Pull the control p.c.b. down, and replace the blown fuse. Table 2-3 Fuse Information
| Reference Number | current | Rating | Otari part number | Used for | |||
|---|---|---|---|---|---|---|---|
| voltage | size(inch mm) | carry | blow | ||||
| FS 801 | 2A | 250V | 1/4 x1 1/4 inch 6.3×32mm | 110% | 135% in 1 hour | FH7E020 | primary circuit |
| FS 701 | " | " | 13/64×45/64 inch 5×20mm | " | " " " | FH7F020 | De servo cap. motor driver |
| FS 702 | " | " | " " " " | " | " " " | " | Brake & pinchroller solenoids |
| FS 703 | " | " | " " " " | " | " " " | " | +5Vdc transport control VU meter lump |
| FS 704 | 1A | " | " " " " | " | " " " | FH7F010 | Relays & Dc servo cap. motor control |
| FS 705 | " | " | " " " " | " | " " " | " | ±15V amplifier |
| FS 706 | " | " | " " " " | " | " " " | " | " |
| --- | --- | --- | --- | --- | --- | ||
| FS701 | 2A | FS705 | 1A | FS706 | 1A | ||
| FS702 | 2A | FS704 | 1A | FS703 | 2A | ||
| CAUTION |
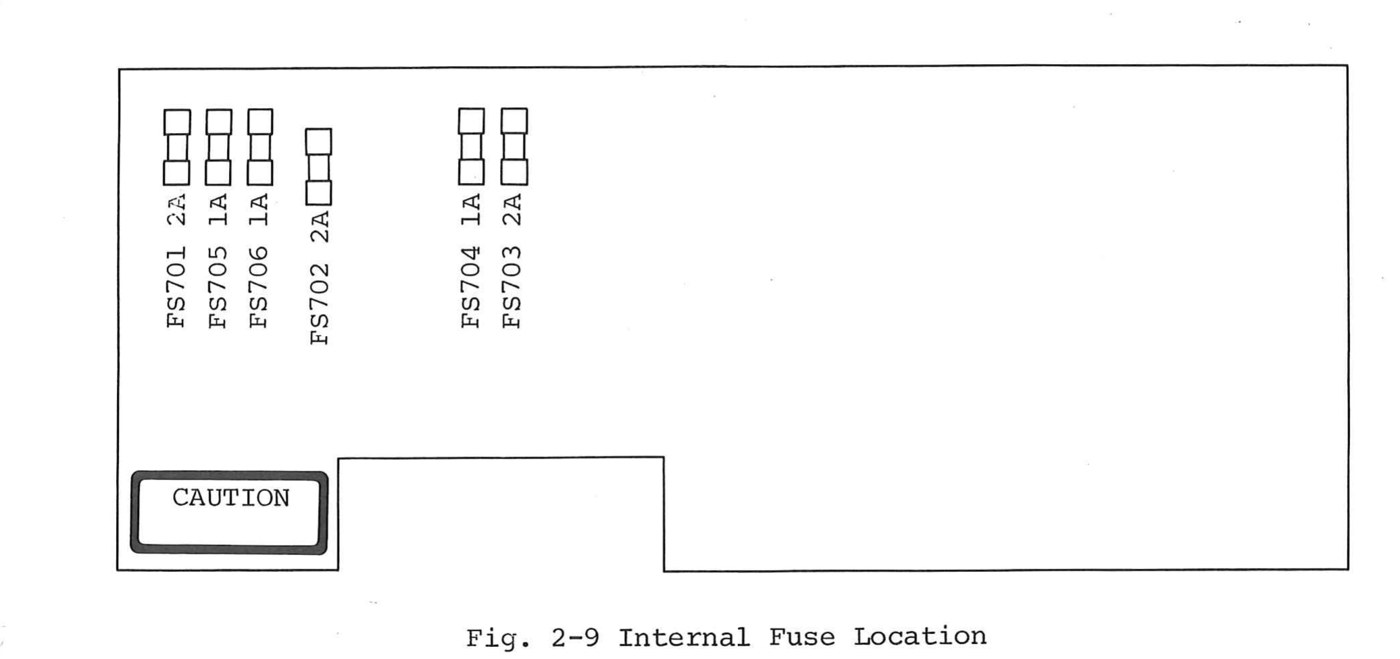 ⤢ zoomFig. 2-9 Internal Fuse Location: the internal fuse board, fuses FS701 to FS706 with their ratings above, and a CAUTION plate at the lower left
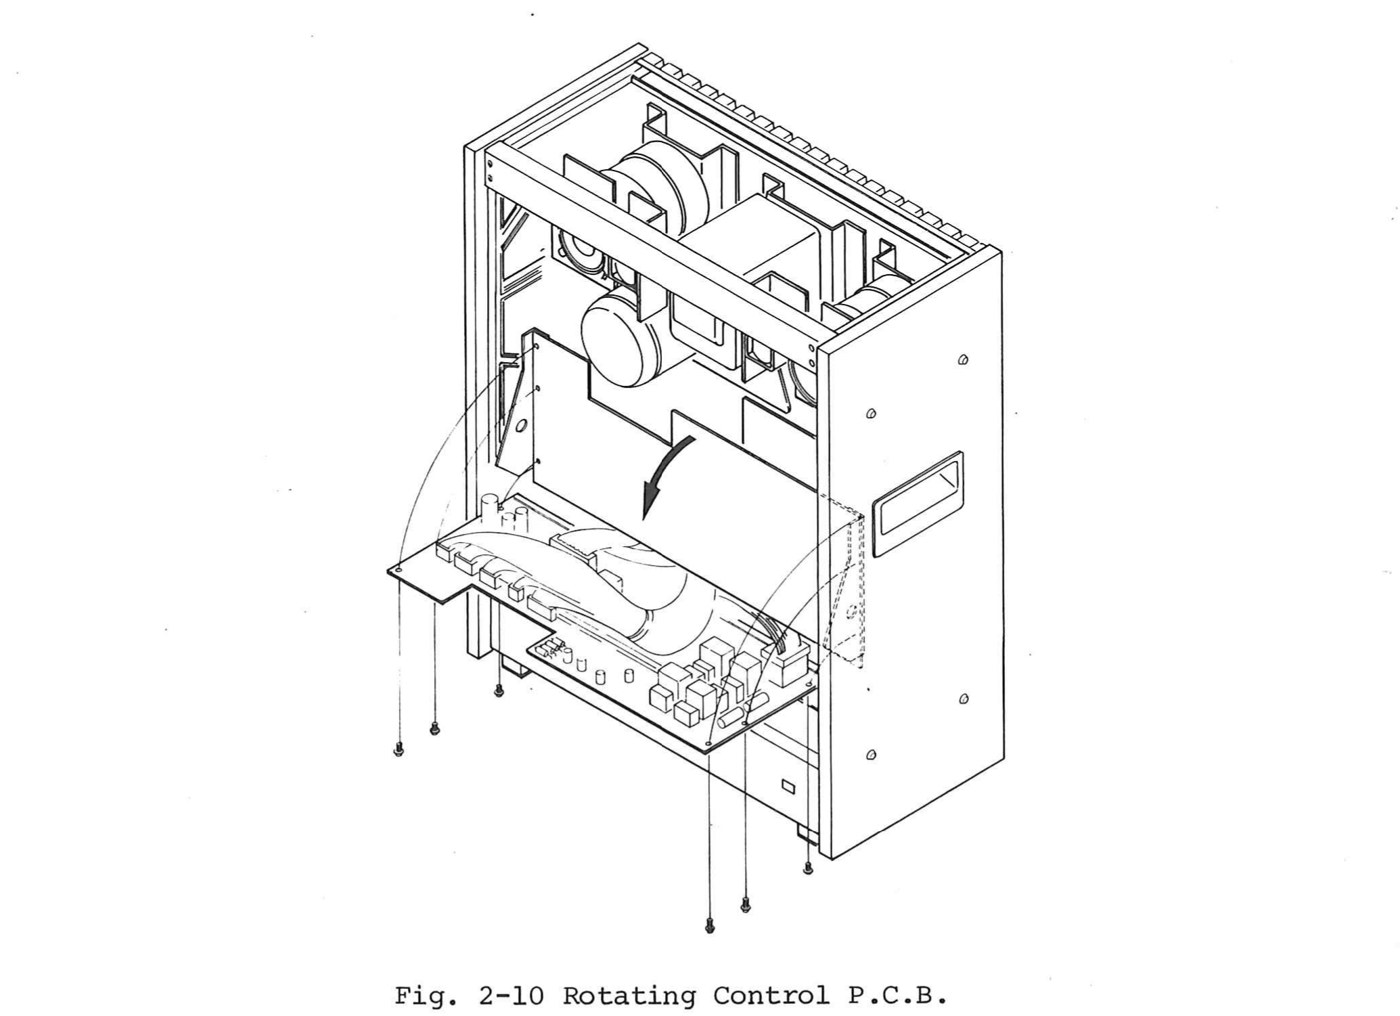 ⤢ zoomFig. 2-10 Rotating Control P.C.B.: the transport seen from behind with the control p.c.b. swung down on its hinge, an arrow showing the rotation