MARK III/4 Instruction and Maintenance Manual — Digital Edition · Part 8 · scan pages 101-110
Major Component Replacement
Prior to replacing major components, perform all the steps for access to the transport.
8-1 REEL MOTOR ASSEMBLY REPLACEMENT↑ TOP
8-1-(1) REEL TABLE REPLACEMENT AND HEIGHT ADJUSTMENT↑ TOP
The reel table may be removed by removing the three cross-recessed screws accessible from the front of the transport.
To adjust the reel table height, loosen the two hex socket head screws in Figure 8-1, adjust the height and retighten the screws.
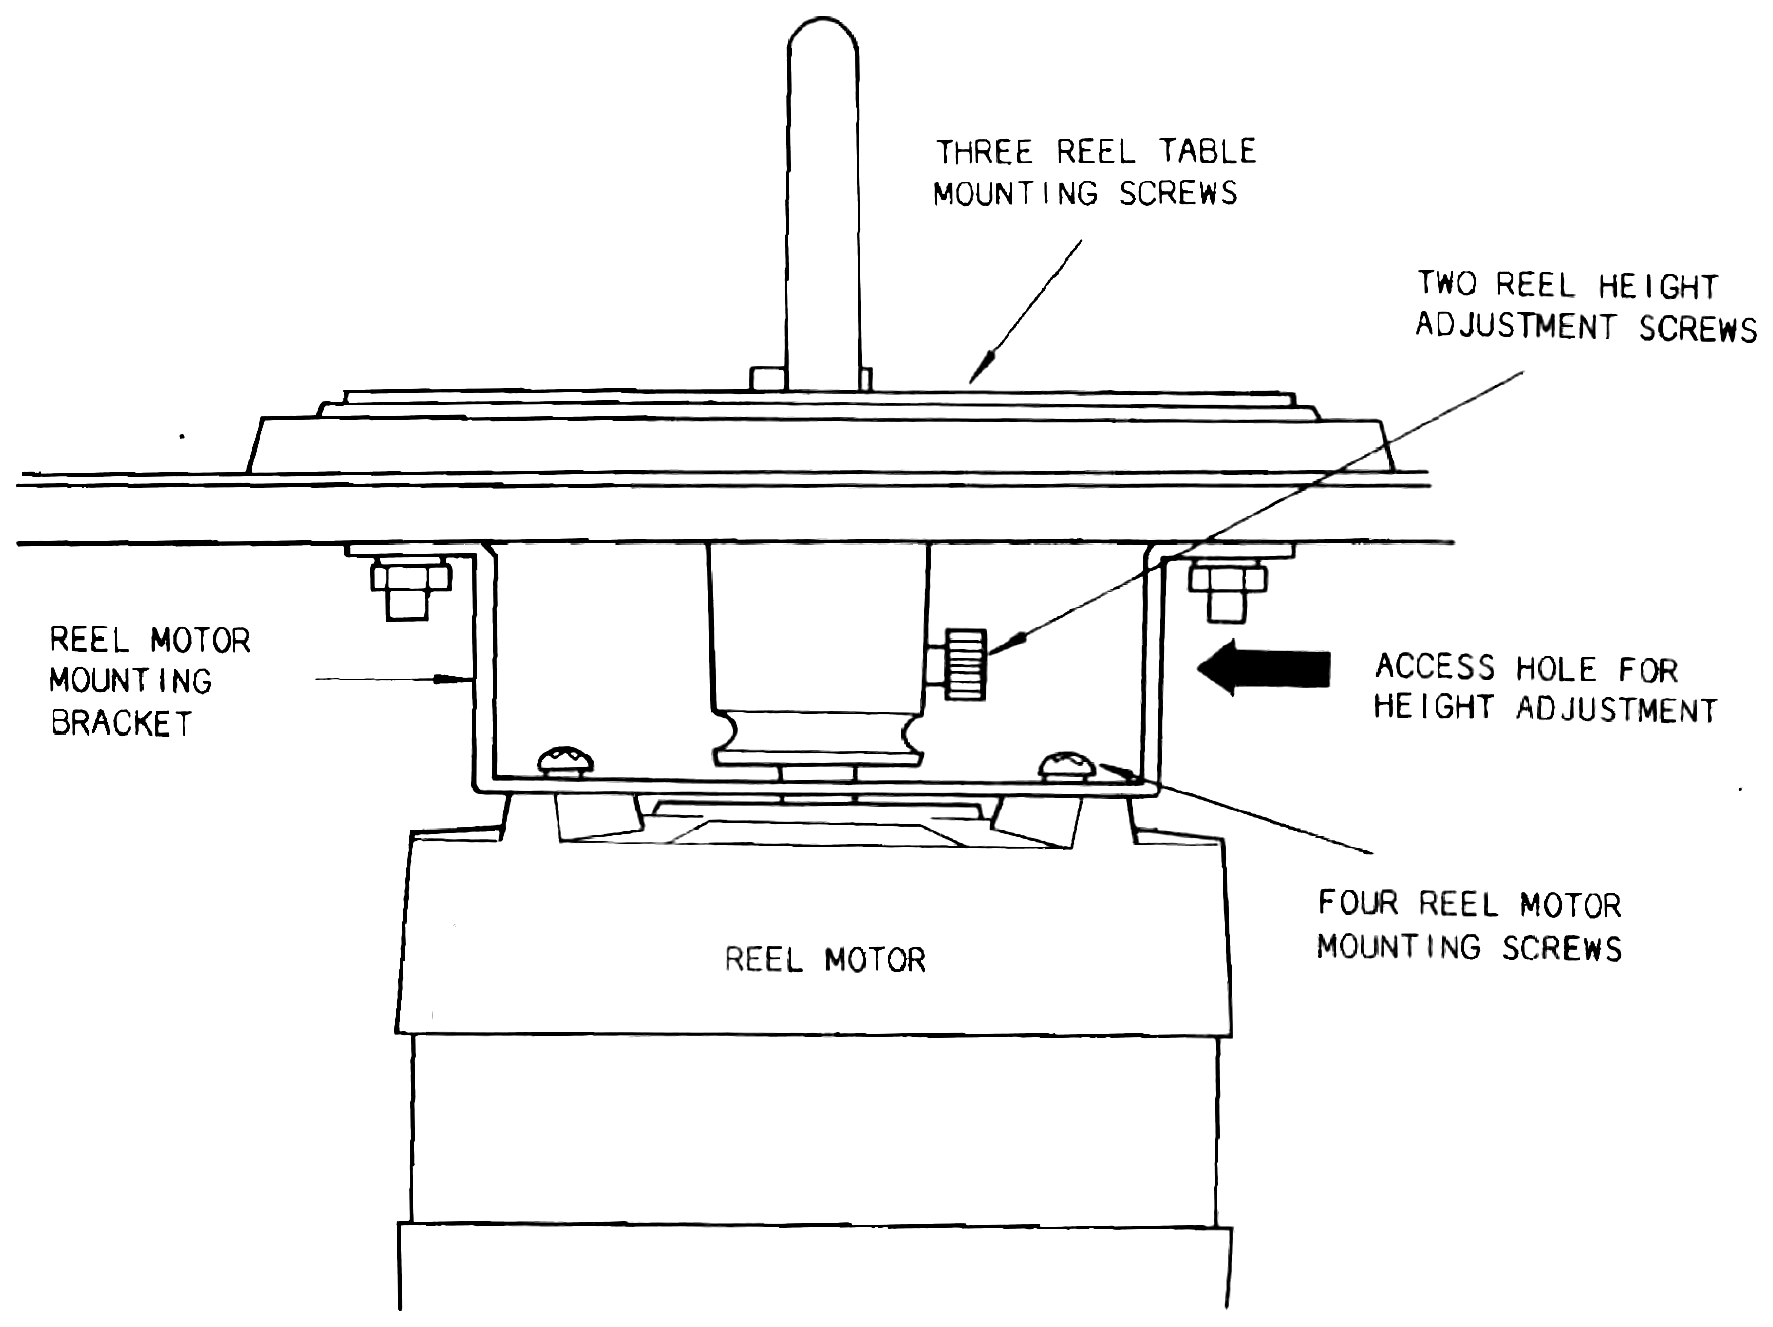 ⤢ zoomA front cross-section of the reel table and motor assembly, with leader lines calling out the three reel table mounting screws, the two reel height adjustment screws and access hole, the reel motor mounting bracket, and the four reel motor mounting screws.
Figure 8-1 Reel Motor Mounting
8-1-(2) REEL MOTOR REPLACEMENT↑ TOP
To replace the supply or takeup motor proceed as follows:
- Loosen the two hex socket head screws on the reel shaft holder (Figure 8-1) and remove the reel table and holder.
- Tag and unsolder the motor leads attached to the printed circuit board.
- Remove the four motor mounting cross-recessed screws, accessible from the front of the transport.
- Remove the brake assembly and the brake drum by removing the four brake assembly mounting screws and two hex socket head screws on the bottom of tne reel motor as shown in Figure 8-2.
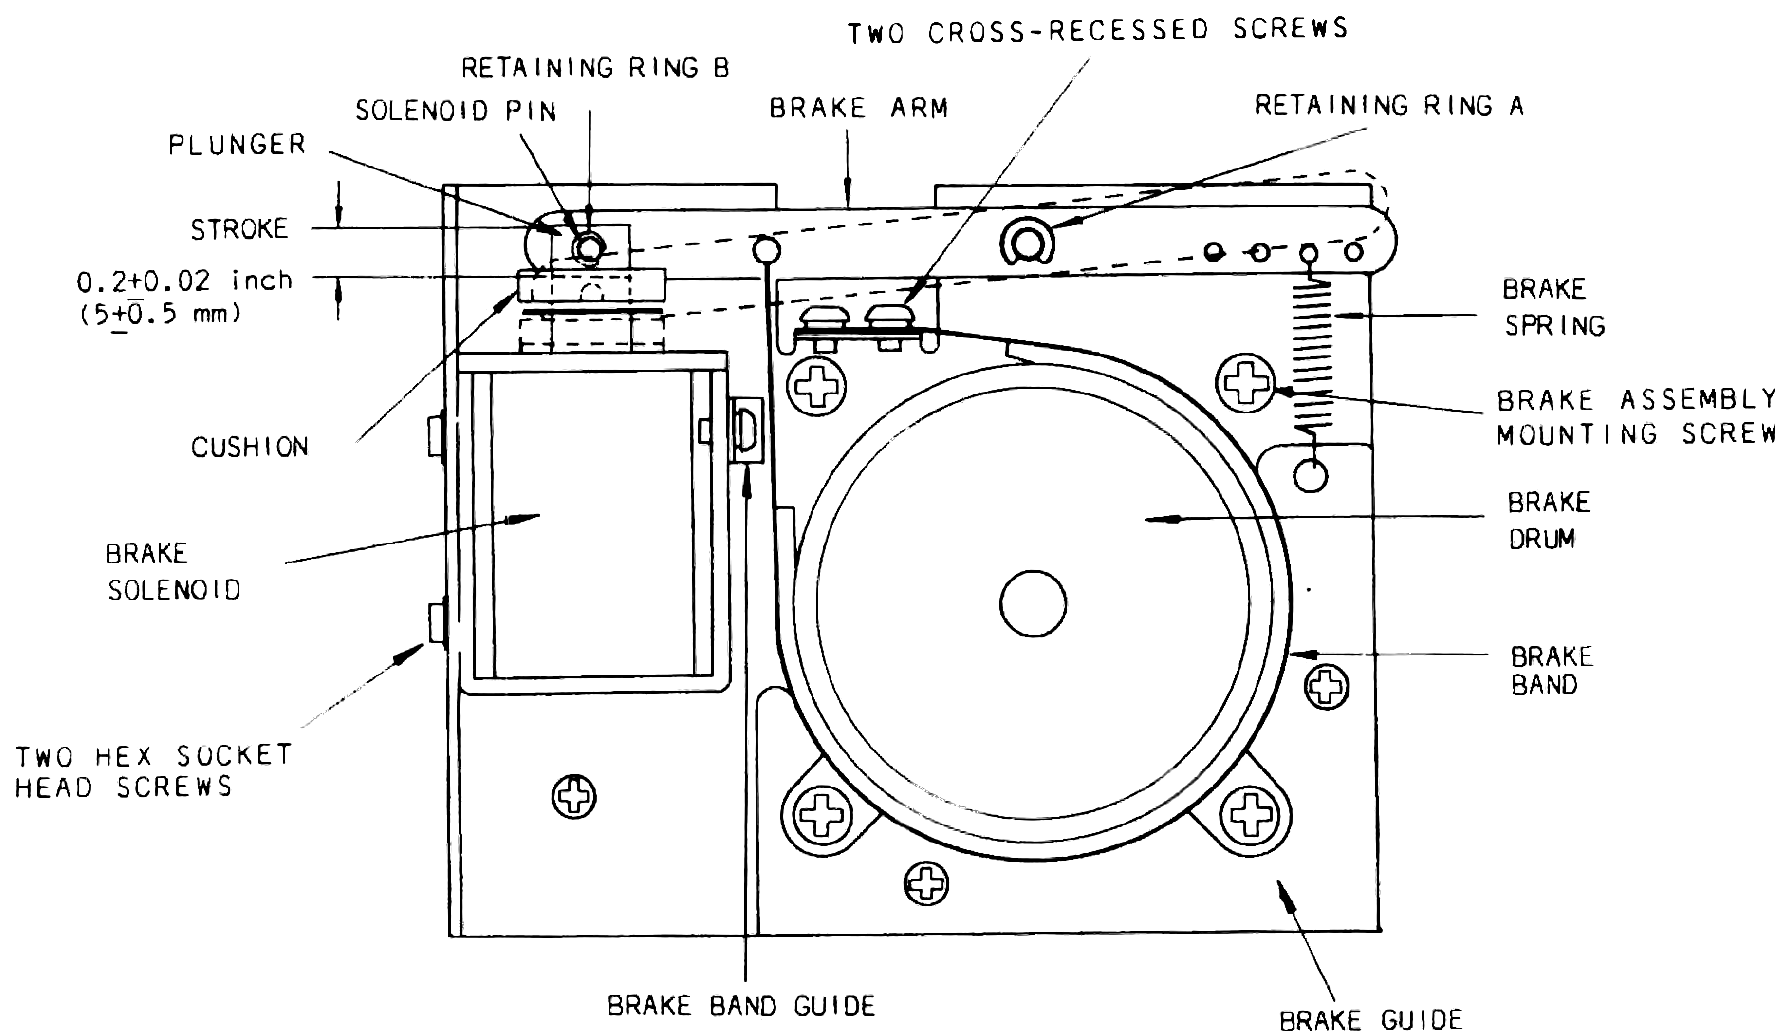 ⤢ zoomA front view of the brake solenoid, plunger and arm assembly mounted beside the brake drum, band and spring, with leader lines labelling each part and the mounting screws.
Figure 8-2 Brake Assembly
8-1-(3) BRAKE ARM ASSEMBLY AND BRAKE SOLENOID REPLACEMENT↑ TOP
When a new brake arm assembly or new brake solenoid is installed (Figure 8-2), it is necessary to position the brake guide and/or brake solenoid to ensure uniform brake band clearance around the brake drum when the solenoid is energized.
Also, the brake solenoid plunger must bottom in the solenoid housing when the solenoid is energized.
When the solenoid is de-energized, the brake band should uniformly contact the drum surface.
After installation, perform the brake adjustment procedure in Section 6 of this manual.
After completion of the adjustments, place the recorder in the play mode for 30 minutes.
Then press the STOP and PLAY pushbuttons alternately to ensure that the solenoid bottoms when it is hot.
To replace the brake arm assembly, proceed as follows:
The brake arm assembly consists of the brake arm and the brake band.
- Remove the retaining rings "A" and "B", and remove the brake spring.
- Remove the two cross-recessed screws, and replace the brake arm assembly.
To replace the brake solenoid, proceed as follows:
- Remove the brake spring.
- Remove retaining ring B on the solenoid pin and remove the solenoid pin.
- Remove the solenoid housing and plunger by removing the two hex socket head screws.
- Install a new solenoid housing and plunger and adjust the solenoid for a 5 ±0.5mm (0.2 ±0.02 inch) plunger stroke by loosing the two hex socket head screws.
8-2 POWER TRANSFORMER REPLACEMENT↑ TOP
To replace the power transformer (refer to EXPLODED VIEW), proceed as follows:
- Tag transformer leads and disconnect the three transformer connectors.
- Remove the four M4 nuts tnat secure the transformer to the transport.
- Install a new transformer in the reverse order of removal, and connect the three transformer connectors.
8-3 CAPSTAN MOTOR REPLACEMENT↑ TOP
The capstan motor should be replaced along with the servo control printed circuit board assembly.
To replace the capstan motor proceed as follows:
- Remove the two hex socket head screws on the head housing cover, and remove the three flat head socket cap screws under the cover. Remove the dust cap from the capstan by turning the dust cap counterclockwise.
- Remove the connector on the servo control printed circuit board assembly located above the capstan.
- Remove the servo control printed circuit board assembly and its mounting plate by turning the two M4 cross-recessed screws (D) and the four cross-recessed screws (B) on the mounting plate.
- Remove the capstan mounting plate and capstan motor by removing the four M4 cross-recessed screws (A) on the mounting plate.
- Remove the capstan motor by removing the three M4 cross-recessed screws (C) on the mounting plate and install a new capstan motor assembly in the reverse order of removal.
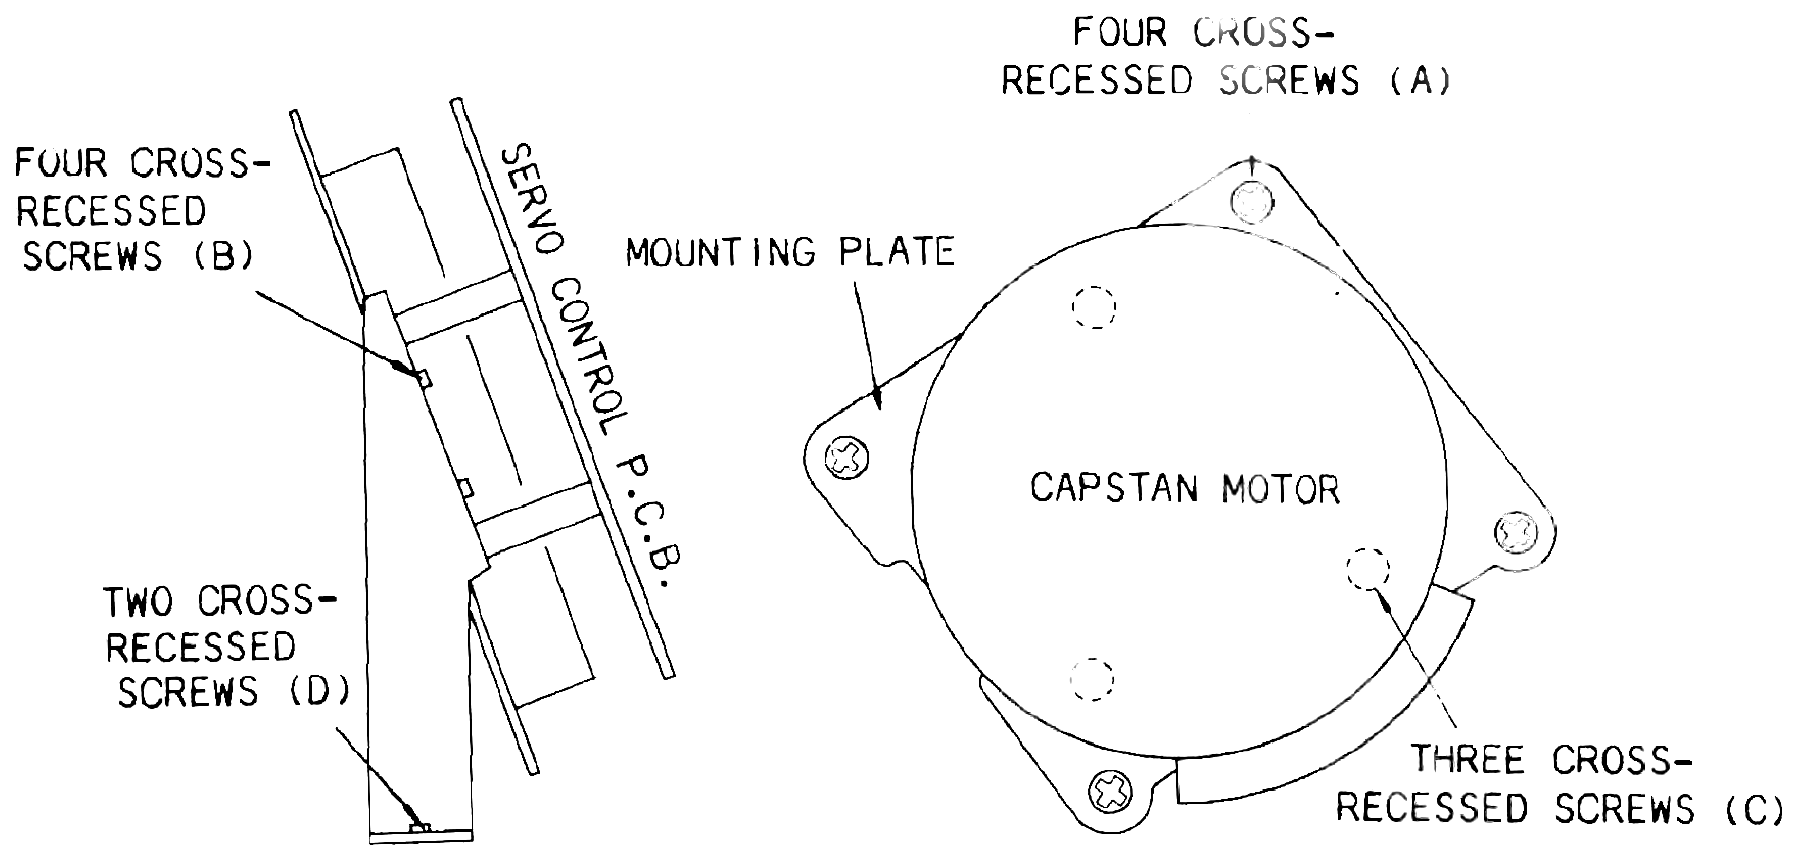 ⤢ zoomTwo exploded views of the DC servo capstan motor assembly: the servo control P.C. board and its mounting screws in profile at left, and the capstan motor's circular mounting plate with its lettered screw positions at right.
Figure 8-3 Location of DC Servo Capstan Motor
8-4 PINCH ROLLER REPLACEMENT↑ TOP
To replace the pinch roller assembly proceed as follows:
- Remove the pinch roller cap by removing the flat head socket cap screw.
- Install a new pinch roller and pinch roller cap in the reverse order.
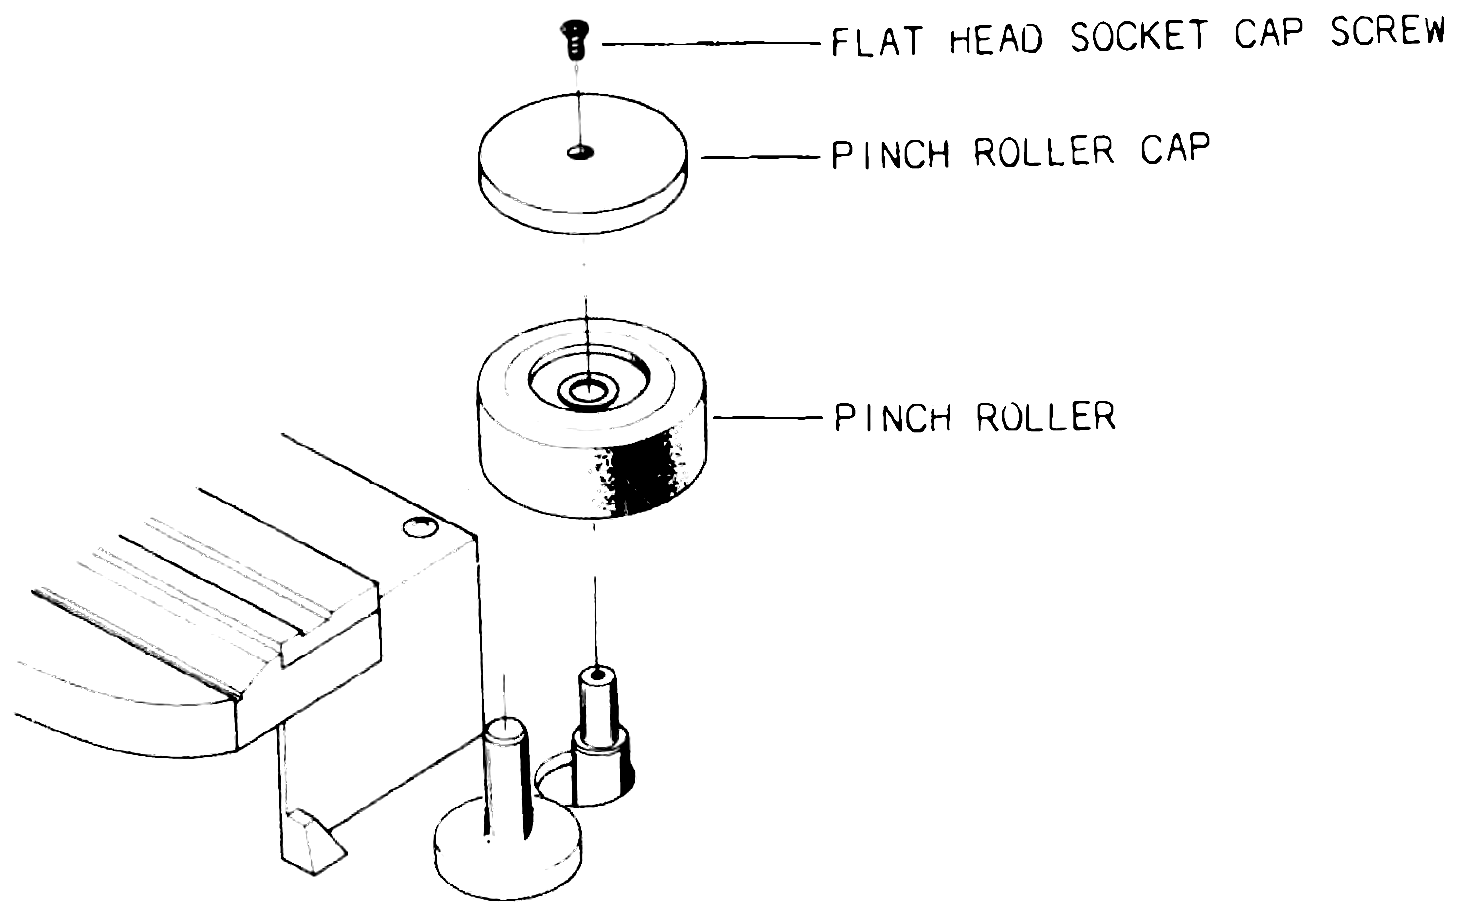 ⤢ zoomAn exploded view of the pinch roller assembly, showing the flat head socket cap screw and pinch roller cap above the pinch roller and its mounting post.
Figure 8-4 Pinch Roller Removal
8-5 HEAD ASSEMBLY REPLACEMENT↑ TOP
This section provides a description of the head assembly, the procedure for changing the head stack, and the adjustment procedure for adjusting head azimuth (tilt), head height, head zenith (perpendicularity), and tape wrap (racking).
These adjustments are required whenever a head stack is replaced.
8-5-(1) DESCRIPTION↑ TOP
The head assembly is mounted on three tape-guide posts and secured in place by the three screws labeled "M" in Figure 8-5.
Each head stack is secured to a bracket by the screws labeled "W".
Each bracket is suspended from the head base by the three spring-loaded screw labeled "H", "A", and "T".
Screws labeled "W" are used to adjust tape wrap.
Screws labeled "H", "A", and "T" are used to adjust height, azimuth, and zenith.
A head stack may be removed and re-lapped (face resurfaced) if the amount of wear is small and only an indication of poor head-to-tape contact is evident.
Poor contact is the result of improper adjustment and is evidenced by the loss of high frequency response of the record or reproduce head, difficulty in achieving bias peak (record head), and insufficient erase head erasure.
8-5-(2) HEAD STACK REPLACEMENT↑ TOP
To change a head stack, proceed as follows:
- Lift the head cover and disconnect the ac power cord.
- Remove the three screws labeled "M" and pull the head assembly out from the head connector.
- Tag and unsolder the leads at the head P.C. Board of the head assembly.
- Remove the head stack by removing the three screws labeled "A", "T", and "H".
- Install a new head stack by tightening the spring-loaded screws up and resolder the leads.
- Paint the head face with a soft crayon, run the tape for about ten seconds, and check the crayon rubbed away by the tape.
If tape wrap is incorrect, adjust the wrap by loosening the screws labeled "W" as shown in Figure 8-5.
Head alignment and the following adjustments are necessary whenever the head is replaced.
-
For reproduce head replacement.
A. Reproduce equalization adjustment.
B. SRL adjustment.
-
For record head replacement
A. Record bias adjustment.
B. Overall frequency response adjustment.
C. Record level adjustment.
-
For erase head replacement.
A. Record bias adjustment.
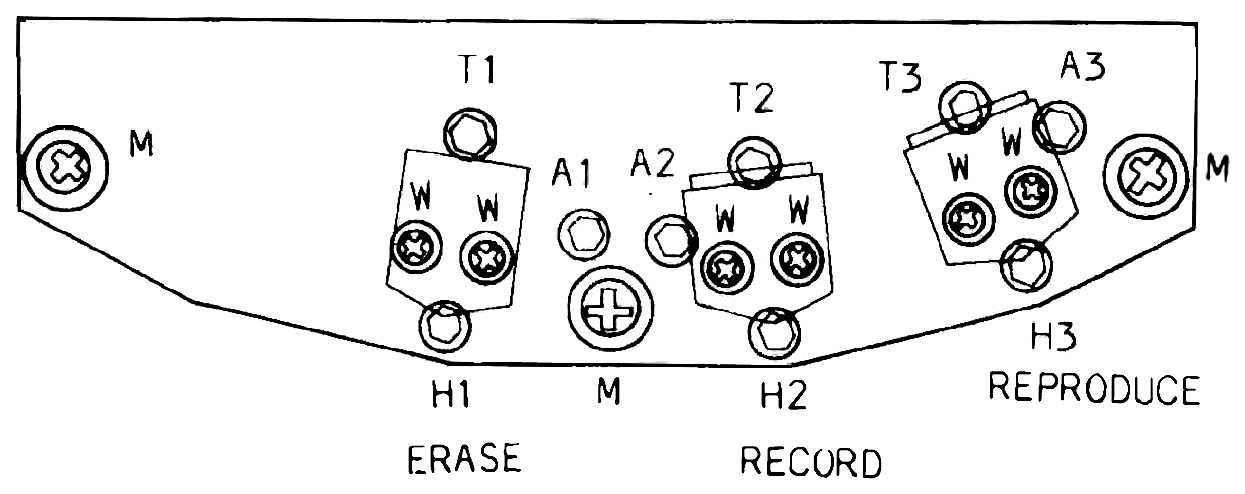 ⤢ zoomA top view of the head base plate with the M mounting screws at each end and the W, H, A and T adjustment screws for the erase, record and reproduce heads labelled across the middle.
Figure 8-5 Head Assembly
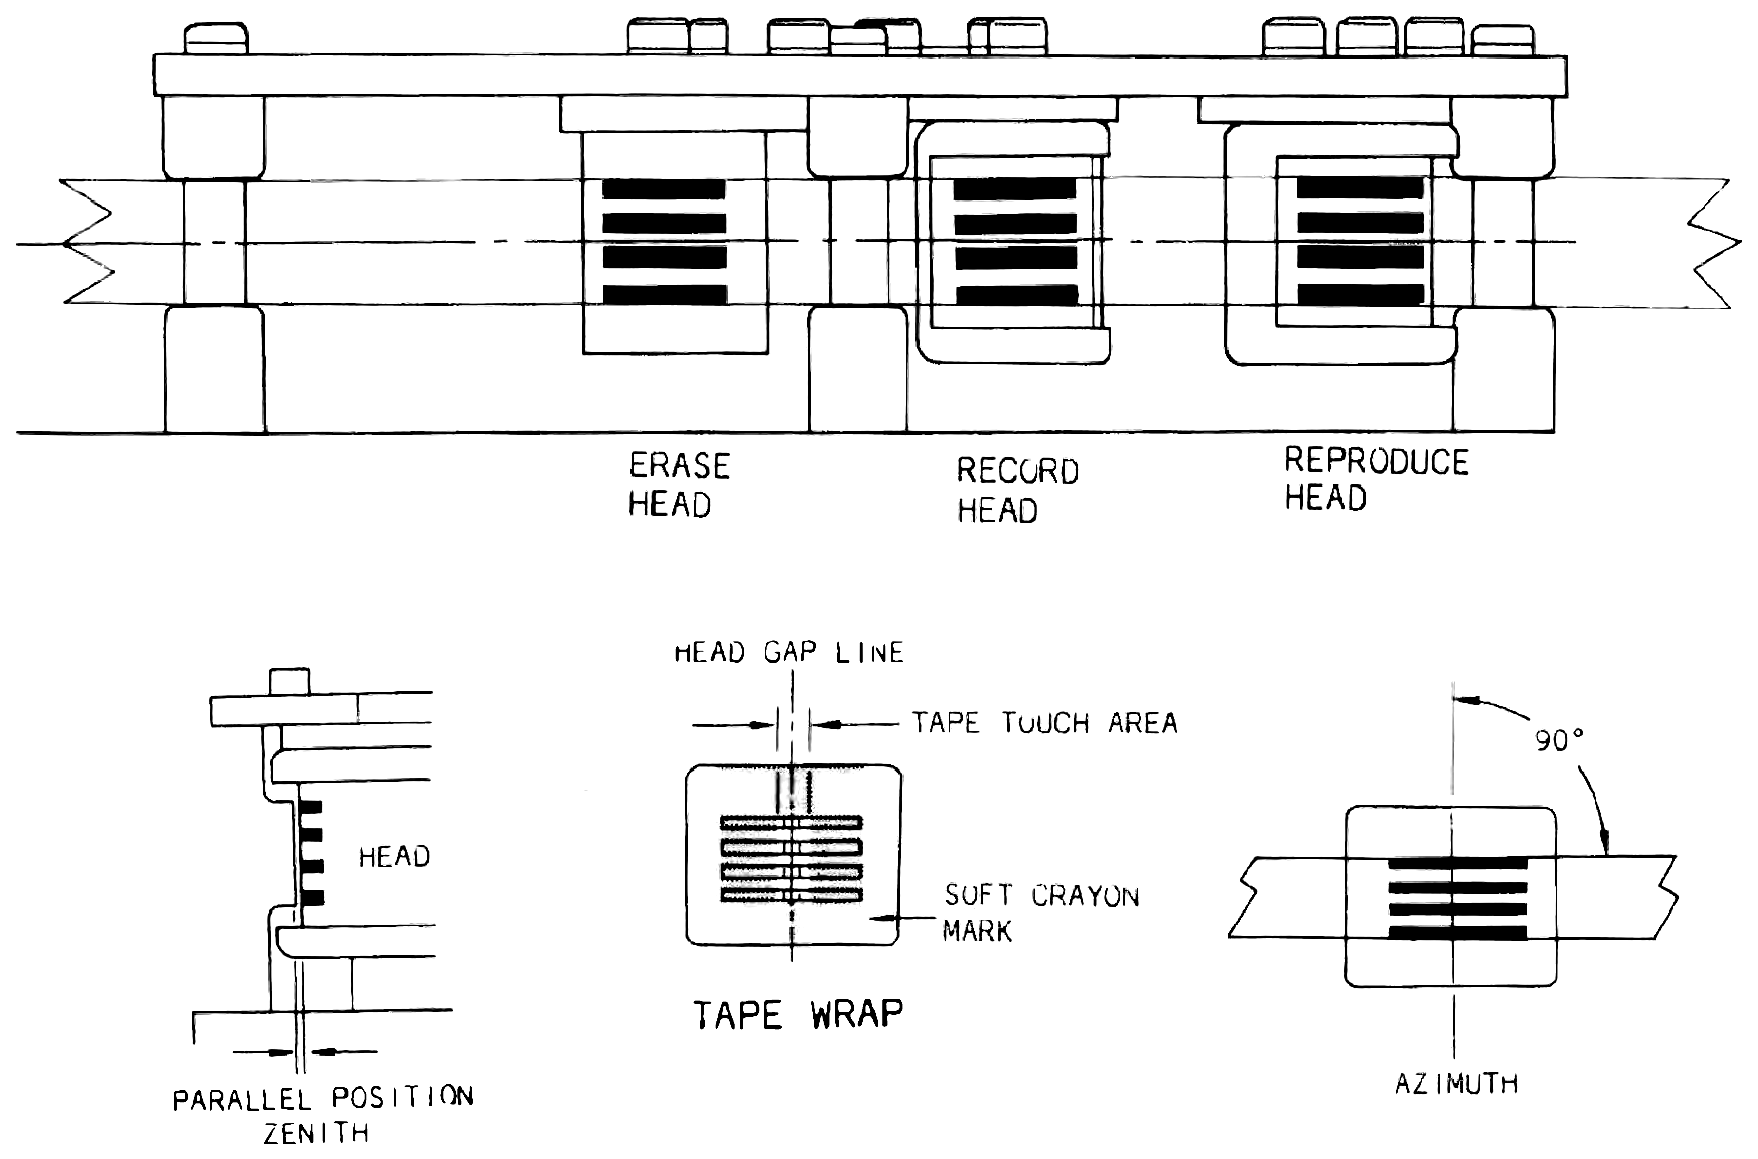 ⤢ zoomA front view of the erase, record and reproduce heads mounted along the tape path, above three detail diagrams labelled parallel position zenith, tape wrap and azimuth.
Figure 8-6 Head Alignment
8-5-(3) RECORD AND REPRODUCE HEAD ADJUSTMENT↑ TOP
Follow the procedure for reproduce system adjustment given in Section 7 of this manual.
For the final adjustment of a record head stack, height and azimuth adjustment may be accomplished in the same manner as for a reproduce head stack, by playing back an alignment tape with the equipment in the selective reproduction mode.
8-5-(4) ERASE HEAD ALIGNMENT↑ TOP
Erase head azimuth is not critical, however wrap angle and head height relative to the record head are important to achieve maximum efficiency.
Poor erasure is often caused by misalignment of the erase head.
Before making any attempt to adjust the erase head stack, an entire electronic alignment procedure (reproduce, record, and bias alignment) should be performed so that the record and reproduce head height are correct, the SRL adjustment is correct, and bias and record levels are properly calibrated.
A temporary erase head adjustment can be accomplished by using a headset or a speaker/amplifier.
However, for precise alignment, a wave analyzer should be used.
Proceed as follows:
- Follow the procedure for erasure test steps 1 through 6 given in Section 7-4-(4).
- Observe the reading on the wave analyzer and turn screw "H" (Figure 8-5) 1/4 turn clockwise.
If the reading decreases, turn the screws "A" and "T" 1/4 turn clockwise.
If the reading increases when "H" is turned 1/4 turn clockwise, turn "H" counterclockwise past the original setting to 1/4 turn counterclockwise.
If the reading decreases, turn screws "A" and "T" counterclockwise by the same amount. - Repeat step 2 in small increments to achieve a minimum reading on the wave analyzer.
Typical amount of erasure should be 70 dB or better.
NOTE:
After screw "H" is turned, be sure to turn screws "A" and "T" the same amount.
- If adjustment of the erase head height alone does not achieve satisfactory erasure, set screws "H", "A", and "T" for a minimum reading on the wave analyzer.
Note that there are two gaps on the face of the erase head.
The trailing gap has the best effect on erasure and must have good contact with the tape.
Loosen screws "W" slightly and rotate the erase head stack for a minimum reading on the wave analyzer.
Tighten screws "W".