MX-5050BII Instruction Manual — Digital Edition · Part 7 · scan pages 78-86
Performance Testing
Performance testing should be made at regularly scheduled intervals (every 150 hours or every month) to ensure that the recorder is performing within specifications. These tests should also be performed whenever the recorder appears to be malfunctioning and following repairs to the equipment that may affect performance.
If the performance test is not successful, proceed to the applicable electronic and mechanic alignment procedure. Refer to previous sections for alignment.
This section provides general test methods for a tape recorder, but space is not enough to describe on all of methods. So please refer to any other published books. Also talk to OTARI or OTARI representative.
7.1 GENERAL NOTICE↑ TOP
It is important to clean and demagnetize the head and tape guiding components before performing the test and alignment procedures. The voltages indicated in this section are for the MX-5050BII-2 model and are at a 1 kHz frequency at reference recording level of 250 nWb/m (The RECORD LEVEL switch on the back panel is in the 'M' position). In the case of IEC equalization, the reference record level is 320 nWb/m (RECORD LEVEL switch is in the 'H' position) that is 1.2 dB above 250 nWb/m. The test equipment listed in Table 4-1 is required for completion of the performance and alignment procedures.
7.2 TEST TAPES↑ TOP
Test tapes are precisely recorded under controlled conditions and must be correctly handled and stored to retain accuracy. Handle the test tapes as follows:
(1) Clean and demagnetize the head and tape guiding components before installing the test tape.
(2) Never store test tapes in areas where there are temperature or humid extremes.
(3) Never run the test tapes on speeds other than a normal play run (never use the rewind or fast forward mode). This is further explained below.
During the alignment procedure, the rewind and fast forward modes should not be used.
After alignment, wind the tape completely on the takeup reel, interchange reels, thread the tape, and place the equipment in the play mode to wind the tape back on its original reel.
After extensive use, high frequency tones may be drop as much as 2 dB. In addition, flutter indication may rise even though actual flutter remains unchanged.
Flutter increase is caused by demagnetization of the recorded signal from repeated plays, tape deformation due to tape tension, changes in temperature and humidity, and increased dropout resulting from tape wear.
7.3 TEST CONDITIONS↑ TOP
The test conditions specified in the following steps are to be met prior to performing the tests. After these test conditions are met, continue with the following procedures for checking overall signal-to-noise, overall distortion, crosstalk, and flutter.
(1) Clean and demagnetize the heads.
(2) Use high quality low-noise tape such as Ampex 456, or Scotch 246, 250, or an equivalent, and bulk erase the blank tape.
(3) Turn the power on and allow the unit to warm up for 20 minutes.
(4) Be sure the head cover is installed for all tests.
7.4 PERFORMANCE TESTS↑ TOP
Before performance testing, an SRL check, reproduce frequency response check, record level check, source level check, an overall frequency response check, and a SEL. REP level check are necessary. Refer to Section V. AMPLIFIER ADJUSTMENTS, in this manual for checking procedures. For performance testing, at first proceed as follows.
Demagnetize and clean the heads and all guiding components.
(1) Set the REEL switch to the appropriate position, and set the EDIT switch to the "out" non-edit position.
(2) Set the LINE OUT switch to 'H', set each RECORD switch to the appropriate position, set each SEL. REP switch to the "out" position, and set each MONITOR switch to the "out" SOURCE position.
(3) Thread a reel of bulk-erased tape onto the transport, set the SRL switch to the SRL position, and push the PITCH CONTROL knob to its fixed position.
7.4.1 OVERALL SIGNAL-TO-NOISE RATIO↑ TOP
The overall signal-to-noise test requires an ASA "A" weighted filter for weighted measurement and a noise filter for unweighted measurement to attenuate noise outside of the audible frequency band. The filter may be built into a small aluminum box as is shown in Fig. 7-1.
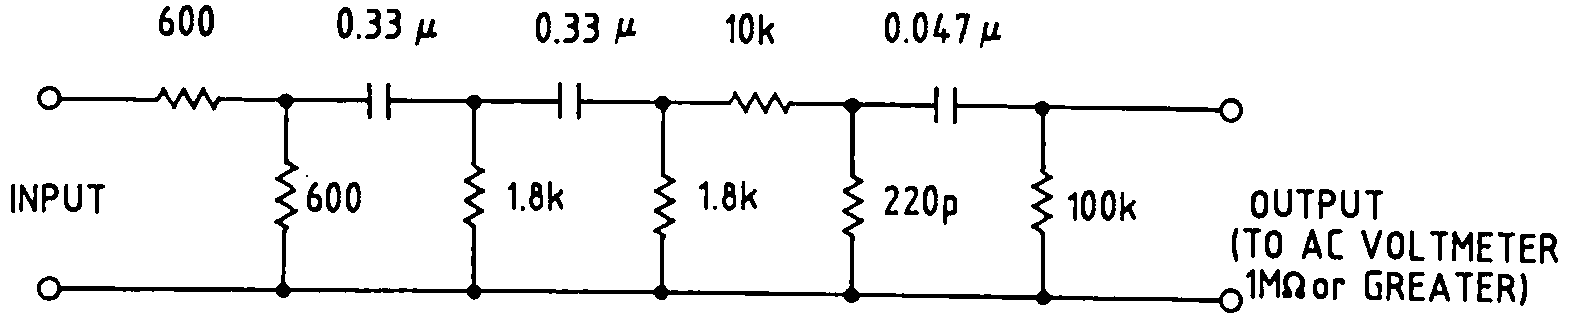 ⤢ zoomSchematic of a five-section RC ladder filter (600 ohm, 0.33 microfarad twice, 10k, 0.047 microfarad) between an input and output pair.
ASA "A" CURVE FILTER (FOR WEIGHTED MEASUREMENT)
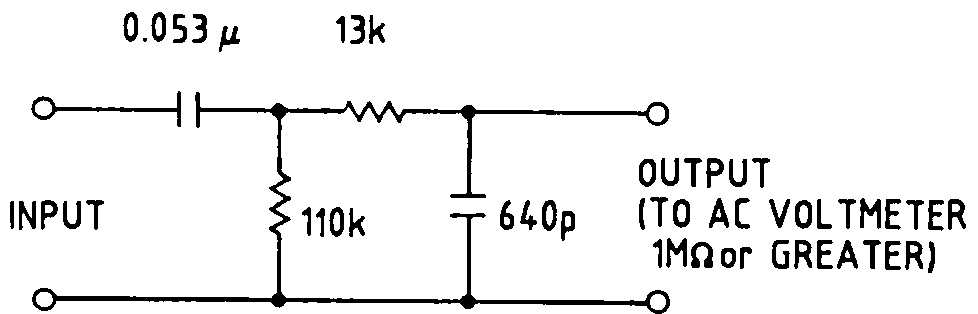 ⤢ zoomSchematic of a two-stage RC filter (0.053 microfarad, 13k, 110k, 640p) between an input and an output pair marked for an ac voltmeter of 1 megohm or greater.
NOISE FILTER (FOR UNWEIGHTED MEASUREMENT)
Fig. 7-1 Filter Schematics
The signal-to-noise ratio depends on the SRL calibration, reproduce equalization, bias calibration, and record equalization. Proceed as follows:
(1) Connect the filter to CH-1 LINE OUT and connect an ac voltmeter to the output of the filter.
(2) Set the reproduce head selector switch on the head assembly to the appropriate position.
(3) Set the SRL switch to the "SRL" position and set the RECORD LEVEL switch to the "M" (250 nWb/m) position.
(4) Hold the TEST OSC push-button depressed and adjust the CH-1 INPUT LINE control for a 0 VU indication on the VU meter. Note the ac voltmeter indication; the ac voltmeter will not read +4 dBm due to the insertion loss of the filter. Release TEST OSC push-button.
(5) Depress the CH-1 MONITOR switch to the "in" TAPE position, and set the CH-1 INPUT LINE and CH-1 INPUT MIC controls to their full counterclockwise positions. Reset the TAPE TIMER to "0000".
(6) Start the record mode and record for one minute. Rewind the tape to the "0000" indication on the timer.
(7) Reproduce the recorded portion and read the noise level on the ac voltmeter.
(8) The signal-to-noise ratio is determined by calculating the difference in readings obtained in step (2) and step (5) plus 6.4 dB (peak recording level - 520 nWb/m- is 6.4 dB above SRL-250 nWb/m).
(9) Repeat steps (1) through (6) for the other channels as required, and change the tape speed to check all signal-to-noise ratios.
Table 7-1 Signal-to-Noise Specifications
| Tape Speed | 1/2 Track Weighted | 1/2 Track Unweighted | 1/4 Track Weighted | 1/4 Track Unweighted | Full Track Weighted | Full Track Unweighted |
|---|---|---|---|---|---|---|
| 15 ips | 66/66 dB | 64/62 dB | 62/62 dB | 60/58 dB | 68/62 dB | 66/60 dB |
| 7 1/2 ips | 68/64 dB | 66/62 dB | 63/62 dB | 61/58 dB | 68/62 dB | 66/60 dB |
| 3 3/4 ips | 66/64 dB | 64/62 dB | 62/62 dB | 60/58 dB | 66/62 dB | 64/60 dB |
Note: 65 dB / 63 dB indicates NAB/IEC equalization.
If signal-to-noise specifications are not met, check and adjust the following items.
- SRL calibration
- RECORD BIAS adjustment
- Reproduce equalization
- Record equalization
- Record and/or reproduce electronics
- Head magnetization
- Magnetic flux of a motor, a soldering iron or a transformer near the recorder.
7.4.2 OVERALL DISTORTION TEST↑ TOP
For accurately checking distortion it is necessary to use an audio oscillator with less than 0.1% distortion and a wave analyzer with an adjustable bandwidth capability. A wave analyzer with too narrow bandwidth may make it difficult to measure harmonics due to flutter components within the transport. Instruments that measure total harmonic distortion will be affected by tape and modulation noise in addition to harmonic distortion. To measure overall harmonic distortion proceed as follows:
(1) Connect a wave analyzer to CH-1 LINE OUTPUT and connect an audio oscillator to CH-1 LINE INPUT.
(2) Set the MONITOR switches to their "in" TAPE positions, set the audio oscillator frequency to 1000 Hz, set the SRL switch to the "SRL" position, and set the RECORD LEVEL switch to the "M" (250 nWb/m) position.
(3) Set the wave analyzer frequency to 1000 Hz, the bandwidth to 100 Hz, and the mode selector switch to AFC.
(4) Start the record mode and adjust the CH-1 INPUT LINE control for a 0 VU reading on the VU meter.
(5) Adjust the fine tuning control on the wave analyzer and adjust the analyzer input level control for a full scale reading of 100%.
(6) Change the wave analyzer tuning control to 2000 Hz and measure the second harmonic content. The second harmonic content should not exceed 0.1%.
(7) Change the wave analyzer tuning control to 3000 Hz and measure the third harmonic content. Third harmonic distortion is dependent upon the type of tape used, and the accuracy of the RECORD BIAS setting. A typical reading for low noise high output tape is 0.4%.
If distortion specifications are not met, check and adjust the following items.
- SRL calibration
- RECORD BIAS adjustment
- Head magnetization
- Record and/or reproduce electronics
7.4.3 CROSSTALK TEST↑ TOP
It is important that blank or well bulk-erased tape should be used for the crosstalk test. To measure crosstalk between channels proceed as follows:
(1) Follow the procedure in the Overall Distortion Test, steps (1) through (5).
(2) Connect a wave analyzer from the output of CH-1 to CH-2 LINE OUTPUT.
(3) Measure the crosstalk in dB.
crosstalk should not exceed that shown in Table 7-2. If crosstalk specifications are not met, record and reproduce head alignment (height and tape contact) is incorrect or the record or reproduce head is defective.
Table 7-2 Crosstalk Specifications
| Track | Crosstalk |
|---|---|
| 1/2 Track | 55 dB |
| 1/4 Track | 50 dB |
| 1/2 Track DIN | 45 dB |
7.4.4 ERASURE TEST↑ TOP
It is important that blank tape should be used in the erasure test. To measure depth of erase, proceed as follows:
(1) Follow the procedure in the Overall Distortion Test, steps (1) through (5). A 1000 Hz signal is being recorded at SRL.
(2) Set the SRL switch to the off position and adjust the OUTPUT control for a -10 VU reading on the VU meter.
(3) Adjust the INPUT LINE control for a 0 VU reading on the VU meter, a 1000 Hz signal is being recorded at 10 dB above SRL. Continue recording for a few minutes.
(4) Disconnect the audio oscillator.
(5) Rewind and reproduce the recorded section. The VU meter reading should be 0 VU. Check the wave analyzer and readjust it as necessary for a full scale reading of 100%.
(6) Press the RECORD push-button to place the recorder in the record mode. As the tape is being erased, adjust the percent scale on the wave analyzer to read the residual 1000 Hz tone.
(7) Repeat the same procedure for the other channels.
(8) The depth of erase should be more than 75 dB (70 dB for DIN version).
If erasure specifications are not met, check and adjust the following items.
- Erase and/or record head alignment (height, tape contact)
- Erase head wear
- Erase head surface cleanliness
- Bias oscillator adjustment.
7.4.5 TAPE SPEED MEASUREMENT↑ TOP
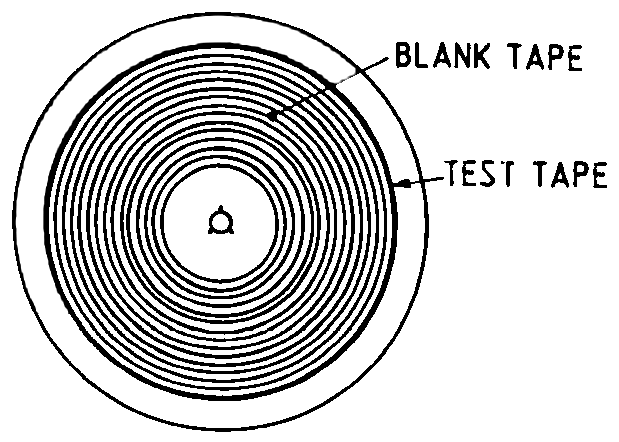
A flutter test tape is used for measuring tape speed. Since tape tension affects tape speed, it is important for accurate measurement that the flutter test tape used is attached to the end of a full reel of blank tape as shown in Fig. 7-2, and is used with the REEL push-button set to the appropriate reel size. Proceed as follows:
(1) Place the PITCH CONTROL in the fixed position and set all RECORD switches to their off "out" positions.
(2) Connect a flutter meter to LINE OUT and set the MONITOR switch to the TAPE position.
(3) Set the SPEED switch to "HIGH" and use the test tape at its appropriate speed.
(4) Attach the test tape to a 10-1/2 inch NAB reel as shown in Fig. 7-2, place the test tape on the supply reel table, thread the tape, and set the REEL switch to the LARGE position.
(5) Place the recorder in the play mode and note the reading on the frequency counter. The reading should be between 2994 and 3006 Hz (3000 Hz ± 0.2%).
(6) Repeat the procedure at a point towards the end of the reel, for a 7 inch EIA reel, and for low tape speeds.
 ⤢ zoomTwo concentric rings of tape wound on a reel hub, the outer ring labeled blank tape and the inner labeled test tape.
Fig. 7-2 Test Tape Loading
(7) If adjustment is necessary, refer to Section 6.4.
If speed accuracy is not within ± 0.2%, check and adjust the following items.
- Pinch roller wear and pressure
- Brakeshoe for brake drum contact
- Tape tension
- Power correctness
- Pinch roller and capstan cleanliness
- Servo control circuit for capstan motor
- Capstan motor.
7.4.6 FLUTTER AND WOW TEST↑ TOP
It is recommended that these checks should be made with reference flutter test tapes which are recorded with precise equipment to produce less than 0.03% rms flutter. Flutter meters are sensitive to amplitude modulation that results from poor head-to-tape contact or from signal dropout. Therefore, clean the heads before starting a flutter and wow test.
The following method is used with a test tape: It is important that the flutter test tape used is attached to the end of a full reel of blank tape as shown in Fig. 7-2, and is used with the REEL push-button set to the appropriate reel size.
(1) Place the PITCH CONTROL to the fixed position and set all RECORD switches to the off "out" position.
(2) Connect a flutter meter to the LINE OUT of the inner track channel and its MONITOR switch should be in the TAPE position.
(3) Set the selector switch of the flutter meter to the NAB weighted position, set the SPEED switch to HI, and use the test tape at an appropriate speed.
(4) Attach the test tape to a 10-1/2 inch NAB reel as shown in Fig. 7-2, place the test tape on the supply reel table, thread the tape, and set the REEL switch to the H position.
(5) Place the recorder in the play mode and note the reading on the flutter meter. The reading should be as shown in Table 7-3.
(6) Repeat the procedure at a point towards the end of the reel, a 7 inch EIA reel, and at low tape speeds.
The following method is used when a test tape is not available:
(1) Connect the oscillator signal output of the flutter meter to an inner channel (not an edge channel) LINE INPUT of the recorder.
(2) Connect the same channel's LINE OUTPUT of the recorder to the signal input of the flutter meter.
(3) Set the SPEED switch to "HIGH", set the SRL switch to the SRL position, set the MONITOR switch to the TAPE position, start the record mode, and adjust the appropriate INPUT LINE control.
(4) Rewind and reproduce the recorded portion, and note the flutter and wow on the flutter meter.
(5) Check the flutter and wow at a low tape speed, and check it at a point towards the end of the reel.
Table 7-3 Flutter and Wow Specifications
| Tape Speed | Flutter and Wow |
|---|---|
| 15 ips | 0.06 % |
| 7.5 ips | 0.08 % |
| 3-3/4 ips | 0.12 % |
Flutter and wow can be caused by any element in the tape path. Excessive flutter and wow may be traced by observing the flutter component on an oscilloscope screen connected to the demodulator output of the flutter meter. If the fluctuation rate observed on the oscilloscope coincides with the rotational elements, such as the supply or takeup reel, capstan or pinch roller, the problem source may be easily traced. Other sources of excessive flutter and wow are:
- Defective capstan servo control
- Damaged capstan motor
- Capstan needs lubrication
- Incorrect tape tension
- Brakeshoe is contacting brake drum.
- Defective tape reels or tape
- Pinch roller is worn or has insufficient pressure, or the pinch roller solenoid is not bottomed.
- Dirty pinch roller and capstan